وظیفه ماشین
Explain repeatability, low lost motion, shaft alignment, thermal behavior, bearing preload, lubrication and inspection scope. These inputs help the quotation reflect the actual machine rather than an industry label.
Precision machinery tends to make small assembly errors more visible. The RFQ should connect tooth geometry with datums, bearing support, backlash expectations and the inspection results needed to release the part.

A precise gear pair still depends on the machine structure that positions it. If the housing or bearing stack moves the gear away from the intended mounting distance, the tooth contact can shift even when both gears were made to the drawing.
When a project has temperature-sensitive behavior, include the operating range and the materials around the gear pair. Do not turn that context into a product-level performance claim unless the ordered configuration has been evaluated for it.
Explain repeatability, low lost motion, shaft alignment, thermal behavior, bearing preload, lubrication and inspection scope. These inputs help the quotation reflect the actual machine rather than an industry label.
هر دو عضو، تعداد یا نسبت دندانهها، دست و اینکه کدام قطعه محرک است را مشخص کنید.
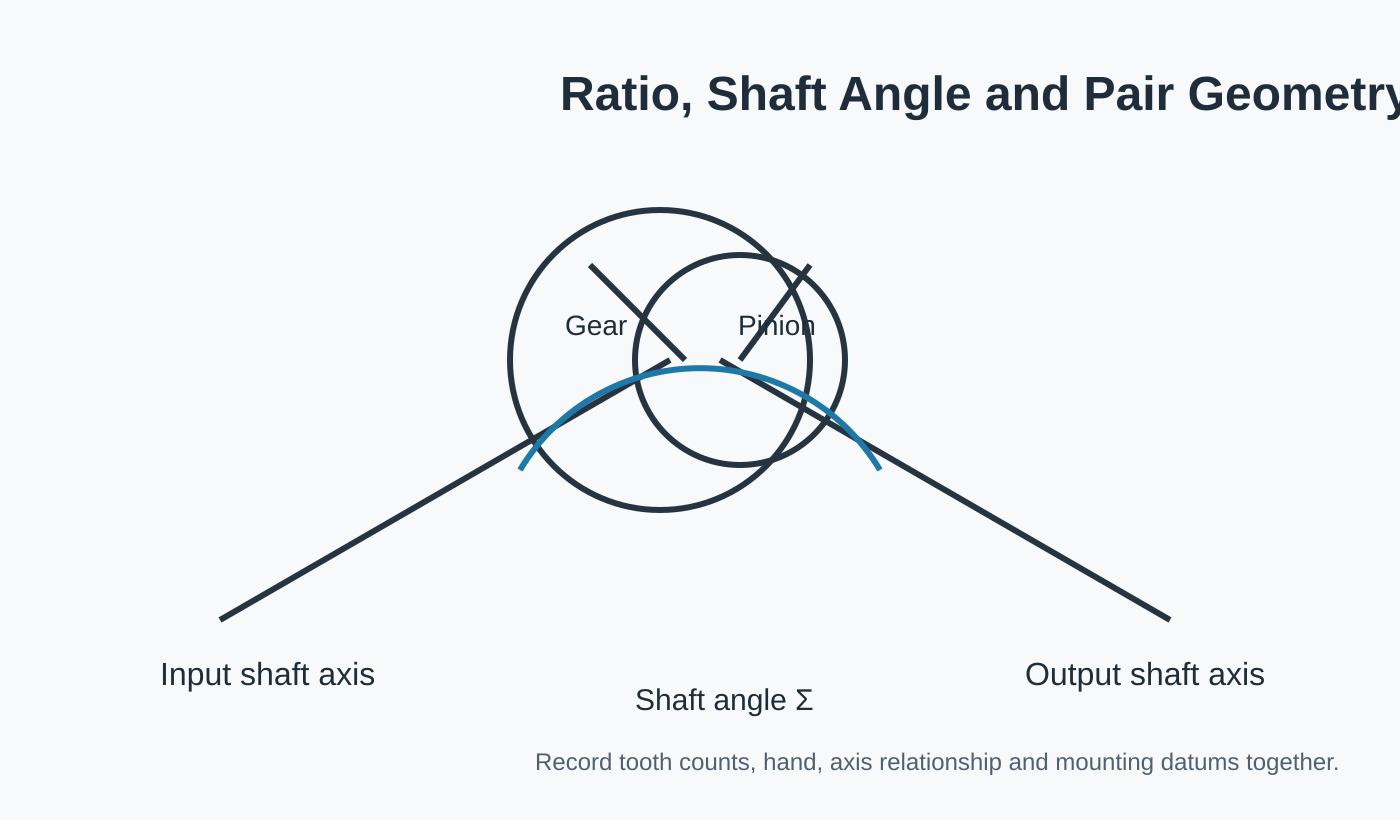
زاویه شفت، مرجعهای نصب، موقعیتهای یاتاقان و هرگونه لقی کنترلشده را نشان دهید.
بررسیهای بازرسی یا تماسی که برای آزادسازی قطعه این دستگاه مهم هستند را بیان کنید.
| منطقه بررسی | چه چیزی ارائه دهیم | چرا مهم است؟ |
|---|---|---|
| حرکت / وظیفه | Repeatability, low lost motion, shaft alignment, thermal behavior, bearing preload, lubrication and inspection scope | انتقال قدرت ثابت را از وظیفه معکوس کردن، ضربه یا حساس به موقعیت جدا میکند. |
| جفت دنده | هویت چرخ دنده + پینیون، نسبت/تعداد دندانهها و عقربه | از بررسی یک جزء بدون هندسه جفت شدن آن جلوگیری میکند. |
| نصب | چیدمان شفت، تکیهگاه یاتاقان، نقاط مرجع محفظه و لقی هدف | قطعه تولید شده را به موقعیتی که در مجموعه خواهد داشت متصل میکند. |
| محیط زیست | زمینه روانکاری، دما و آلودگی | بدون ایجاد ادعاهای سطح ماشین، از بررسی عملی مواد، پرداخت و خدمات پشتیبانی میکند. |
| بازرسی | تلرانسهای رسم، پرداخت دندانه و سوابق مورد نیاز | تعریف میکند که خریدار برای پذیرش پیکربندی سفارش داده شده از چه چیزی استفاده خواهد کرد. |
Tighter numbers are not automatically better if the machine cannot hold them. Define the values that the assembly can control, and state which surface or axis is the reference for each acceptance dimension.
Ground or custom matched pairs are typical starting points for higher-control applications. A pinion shaft can reduce separate joint interfaces when the design intentionally integrates the shaft and pinion.
If a precision machine assembly still has open geometry or duty inputs, mark those items for review. An explicit unknown is safer than filling the drawing with an assumed standard value.
Replacement spiral bevel gear work begins by separating original design information from service wear. A damaged tooth, distorted bore or shifted contact pattern can describe the failure, but…
مشاهده پیکربندی →
A heavy-duty spiral bevel gear pair should be reviewed from the complete operating duty. Peak load, continuous load, shock events, reversals, bearing support and lubrication can all matter…
مشاهده پیکربندی →
Integrating the spiral bevel pinion with a shaft reduces separate joints, but it makes bearing journals, shoulders, splines, threads and tooth datums part of one manufacturing problem. The…
مشاهده پیکربندی →
A spiral miter gear set uses equal tooth counts to transmit motion between intersecting shafts without intentionally changing speed ratio. Equal ratio simplifies one part of the selection,…
مشاهده پیکربندی →
Ground spiral bevel gears require more than adding a grinding operation to a normal gear. The datum scheme, pre-grind geometry, heat treatment, grinding allowance and final inspection have…
مشاهده پیکربندی →
A custom spiral bevel gear set is built around project-specific geometry rather than a public stock table. The useful definition includes both members of the pair, the axis…
مشاهده پیکربندی →When the precision machine assembly drawing controls material or heat treatment, include the exact requirement. If those choices remain open, describe the duty and leave material/process selection for review.
Photos of the precision machine assembly help establish orientation and condition, but they do not define tooth geometry or mounting datums. Add the mating member, drawing data and measurements taken from controlled assembly references.
For the precision machine assembly, send the assembly information that controls shaft relationship, mounting datums and interfaces. Unrelated machine details can be omitted when they have no effect on gear selection or inspection.
For the precision machine assembly, separate prototype/sample quantity from expected repeat demand. This keeps tooling, inspection and production planning tied to the real purchasing stage.
هرچه رابطه جفتسازی و مبنای مونتاژ واضحتر تعریف شوند، پیکربندی سریعتر قابل بررسی خواهد بود.
حداقل مقدار سفارش (MOQ) بسته به نوع محصول، مسیر تولید و ارزش کل سفارش انعطافپذیر است. پروژههای جدید مناسب ممکن است ۱ تا ۵ قطعه نمونه را با قیمت نمونه درخواست کنند. مدلهای ترکیبی را میتوان زمانی که کل سفارش تقریباً به ۱۵۰۰ دلار آمریکا برسد، ترکیب کرد. سفارشهای ۱ تا ۲ قطعهای قابل بررسی هستند، اگرچه هزینه واحد معمولاً بالاتر است.
بازههای برنامهریزی معمول برای قطعات استاندارد ۱۰ تا ۲۵ روز کاری، برای اجزای سفارشی ۲۰ تا ۴۵ روز کاری و برای تجهیزات یا مجموعههای پروژهای ۴۵ تا ۱۲۰ روز کاری است. EXW، FOB، CIF و DAP معمولاً پشتیبانی میشوند؛ FCA، CFR، CPT، CIP و DDP را میتوان برای حمل و نقل مورد بحث قرار داد.