機械作業
Explain reversing frequency, acceleration, inertia, positional repeatability, shaft support and service interval. These inputs help the quotation reflect the actual machine rather than an industry label.
In automated equipment, the gear set rarely works alone. Motor, coupling, bearings, shafts and the downstream mechanism all influence how reversal and torque are seen at the teeth. A useful RFQ describes that motion profile instead of treating the gear as a static catalogue item.
If the gear is part of a servo-driven mechanism, explain whether the downstream process depends on repeatable angular position or simply on power transfer. That distinction changes which inspection results are useful to the buyer.
Explain reversing frequency, acceleration, inertia, positional repeatability, shaft support and service interval. These inputs help the quotation reflect the actual machine rather than an industry label.
両方のメンバー、歯数または比率、手、およびどのコンポーネントが駆動するかを特定します。
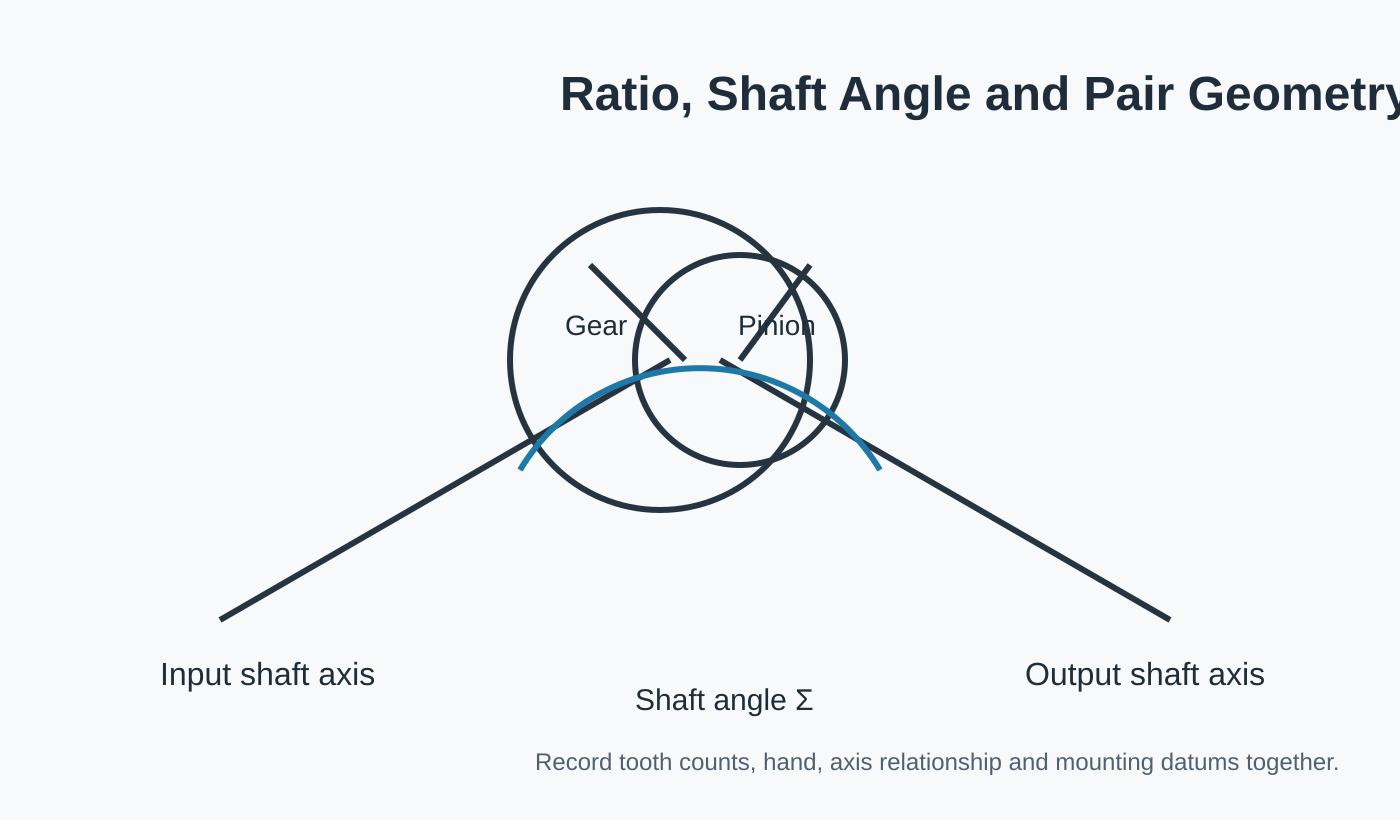
シャフト角度、取り付け基準、ベアリング位置、および制御可能なバックラッシュを示してください。
この機械の部品を出荷するために重要な検査または連絡確認事項を明記してください。
| レビューエリア | 提供すべきもの | なぜそれが重要なのか |
|---|---|---|
| 動作/任務 | Reversing frequency, acceleration, inertia, positional repeatability, shaft support and service interval | 定常的な動力伝達と、逆転、衝撃、または位置制御を必要とする動作を分離します。 |
| ギアペア | ギア+ピニオンの識別、比率/歯数、手 | 一方の部品が、その嵌合形状なしにレビューされることを防ぎます。 |
| 取り付け | シャフト配置、ベアリング支持、ハウジング基準点、および目標バックラッシュ | 製造された部品を、組み立て後の所定の位置に取り付けます。 |
| 環境 | 潤滑、温度、汚染の状況 | 機械レベルの主張を捏造することなく、実用的な材料、仕上げ、およびサービスに関するレビューをサポートします。 |
| 検査 | 図面公差、歯面仕上げ、および必要な記録 | 購入者が注文された構成を受け入れるために使用するものを定義します。 |
Backlash that is acceptable in a continuous conveyor can be noticeable in a mechanism that changes direction repeatedly. Do not assume a generic backlash value; use the machine requirement and the mounting geometry that can actually maintain it.
Ground or custom pairs are a natural starting point for motion-sensitive mechanisms, while a miter set can suit compact 1:1 direction changes when the ratio and axis relationship are fixed.
If a robotic axis or automated positioning cell still has open geometry or duty inputs, mark those items for review. An explicit unknown is safer than filling the drawing with an assumed standard value.
スパイラルベベルギアの交換作業は、元の設計情報と使用による摩耗情報を分離することから始まります。歯の損傷、穴の歪み、接触パターンのずれなどが故障の原因として挙げられますが、…
設定を表示 →
高負荷用スパイラルベベルギアペアは、運転条件全体を考慮して検討する必要があります。ピーク負荷、連続負荷、衝撃、逆転、ベアリング支持、潤滑など、すべてが重要となる可能性があります。
設定を表示 →
スパイラルベベルピニオンをシャフトに一体化することで、個別のジョイントは減りますが、ベアリングジャーナル、肩部、スプライン、ねじ山、歯面基準点が1つの製造上の問題の一部となります。
設定を表示 →
スパイラルマイターギアセットは、歯数が等しいため、意図的に速度比を変更することなく、交差するシャフト間で運動を伝達します。速度比が等しいことで、選定の一部が簡素化されます。
設定を表示 →
研削加工されたスパイラルベベルギアは、通常のギアに研削加工を追加するだけでは済みません。基準面、研削前の形状、熱処理、研削代、最終検査など、多くの要素が考慮されています。
設定を表示 →
カスタムスパイラルベベルギアセットは、公開されている既製テーブルではなく、プロジェクト固有の形状に基づいて構築されます。便利な定義には、ペアの両方の部材、軸、…が含まれます。
設定を表示 →When the robotic axis or automated positioning cell drawing controls material or heat treatment, include the exact requirement. If those choices remain open, describe the duty and leave material/process selection for review.
Photos of the robotic axis or automated positioning cell help establish orientation and condition, but they do not define tooth geometry or mounting datums. Add the mating member, drawing data and measurements taken from controlled assembly references.
For the robotic axis or automated positioning cell, send the assembly information that controls shaft relationship, mounting datums and interfaces. Unrelated machine details can be omitted when they have no effect on gear selection or inspection.
For the robotic axis or automated positioning cell, separate prototype/sample quantity from expected repeat demand. This keeps tooling, inspection and production planning tied to the real purchasing stage.
接合関係と組立基準が明確に定義されていればいるほど、構成の確認は迅速に行える。
最小発注数量(MOQ)は、製品の種類、製造方法、および注文総額によって柔軟に対応可能です。適切な新規プロジェクトでは、サンプル価格で1~5個のサンプルを注文できます。注文総額が約1,500米ドルに達した場合、複数のモデルを組み合わせることができます。1~2個の注文も検討可能ですが、通常は単価が高くなります。
標準部品の一般的な納期は10~25営業日、特注部品は20~45営業日、プロジェクト型機器または組立品は45~120営業日です。EXW、FOB、CIF、DAPは一般的に対応可能ですが、FCA、CFR、CPT、CIP、DDPについてはご相談ください。